Packaging Plant Maintenance Software for Converting Lines
Published on 10/21/2026 • Updated on 10/23/2026
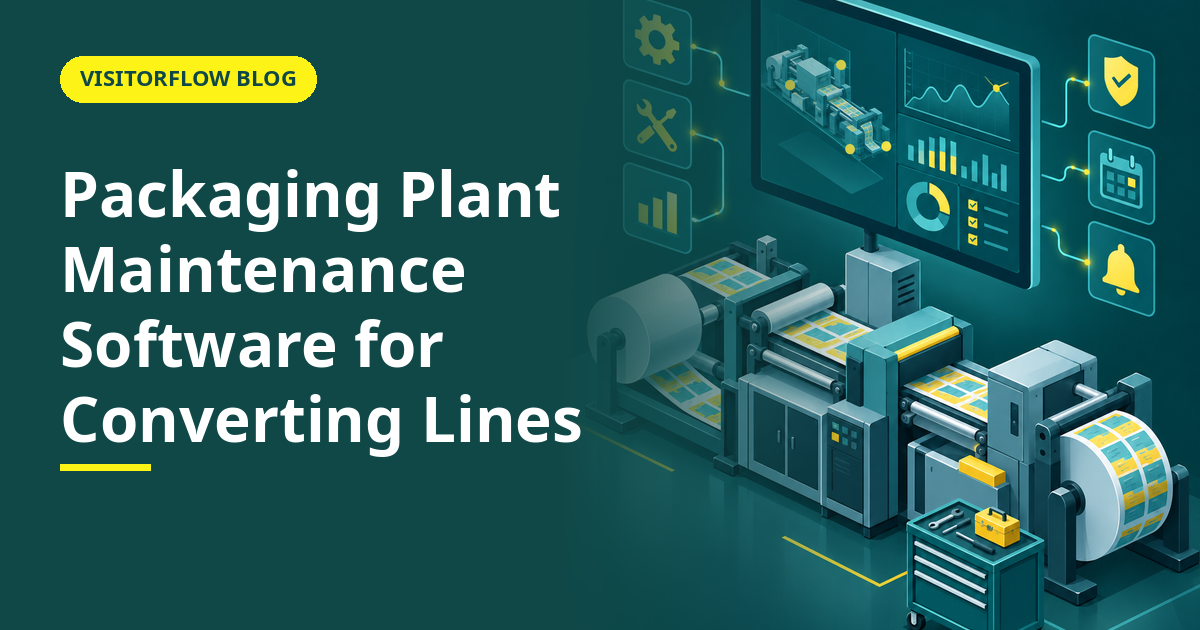
A flexible packaging plant in Daman runs two rotogravure presses and six slitting machines for FMCG customers. Press 1's registration has been drifting a hair on the last colour for a week; the operator compensates and carries on, because stopping a gravure press to chase a hair is how you miss dispatch. Then the customer's incoming QC rejects 40,000 printed rolls for registration out of tolerance, and the hair turns out to be a worn impression roller bearing that a planned half-hour swap would have fixed.
This guide covers maintenance management for packaging and converting plants: the press-to-dispatch asset chain, why print quality drift is a maintenance signal, and how a ticketing habit carries the operator's compensation notes to maintenance before the customer carries them back. For the general maintenance workflow, our guide to the maintenance ticketing system covers the basics; this article is about the packaging plant's specific machinery.
On this page
The press-to-dispatch chain
A packaging plant is a chain where each stage hands quality to the next. Printing presses (gravure or flexo) wear impression rollers, doctor blades, anilox rolls and bearings, and their failure mode is print drift the operator compensates away. Laminators and coaters wear nip rollers and heating systems. Slitters, rewinders and pouch machines wear blades, knives and seals on running hours. Extrusion lines for film wear screws and dies over months. And the compressed air, chillers and exhaust systems serve all of them while scaling and leaking quietly.
What this chain means for the maintenance system:
- Quality drift is a maintenance ticket. Registration drift, coat weight variation and seal inconsistency are machine wear announcing itself; the operator's compensation note should become a ticket the same shift.
- Blades and seals live on running hours. Slitter blades, sealing jaws and doctor blades have known service lives; PM belongs on hours, not the first of the month.
- Changeovers hide inspection windows. Job changes are the natural moment for the five-minute checks that catch wear early, and they need a checklist ticket to actually happen.
- Customer complaints arrive weeks late. The roll rejected at the customer's QC was printed three weeks ago; only per-asset history connects the complaint back to the drift that caused it.
Key idea: In a packaging plant the machine tells you it is wearing by printing slightly worse; the maintenance system that listens to quality drift is the one that ships fewer rejections.
Logbook vs ERP module vs a ticketing system
Most plants run a press logbook for job data and a maintenance diary for breakdowns; larger units have an ERP module that the maintenance team treats as a stores system. The comparison shows where each lands when the customer complaint lands.
| What the plant needs | Logbook plus diary | ERP maintenance module | VisitorFlow Maintenance (ticketing) |
|---|---|---|---|
| Drift observation reaches maintenance | Margin note, if the page survives | Operator has no ERP login | One-minute ticket with photo from the press side |
| Blade and seal PM on running hours | Operator's habit, varies by person | Calendar only | Hours-based triggers per machine |
| Complaint traced to machine condition | Argument and guesswork | Job data, no machine health | Per-asset ticket history by date range |
| Changeover inspection actually happens | When the crew has time, which is never | Not its job | Checklist ticket per changeover |
Catch the drift before the customer does
VisitorFlow Maintenance puts one-minute tickets on the operator's phone and PM schedules on running hours, per machine.
Explore Maintenance SoftwareSetting it up in three moves
Move 01
Register the chain as linked assets
Presses, laminators, slitters, pouch machines, extruders and utilities each get asset records with running-hour counters. A quality complaint against a job lot can then be traced to the machine's ticket history in that date range: the drift, the fix, the part.
Move 02
Make drift a ticket the same shift
When the operator compensates for anything (registration, tension, seal temperature), that compensation becomes a one-minute ticket. Maintenance sees the pattern across three shifts instead of discovering a worn bearing from the customer's QC report.
Move 03
Bolt inspection onto changeovers
Every job change triggers a five-minute checklist ticket: doctor blade condition, roller surface, blade sharpness, seal jaw cleanliness. The window already exists; the ticket makes sure the looking happens inside it.
The PM calendar by asset family
A workable packaging PM calendar runs three trigger types. Running-hour items: slitter blades, sealing jaws, doctor blades, anilox cleaning, bearing lubrication. Calendar items: chiller water treatment, compressor service, exhaust duct cleaning, electrical panel thermography. Event items: the changeover checklist and the post-complaint investigation. A ticketing system holds all three against the right machine and turns due items into tickets instead of a chart the day shift walks past.
The discipline that makes it stick: tickets close with what was done and which parts went in, and the monthly review reads the repeat-offender list. Six months later, the plant can answer which machine causes the most compensation tickets, whether blade changes happen early "to be safe", and what the last three customer complaints had in common mechanically.
Reader Q&A
Won't operators hide compensation instead of ticketing it?
Only if compensation is treated as blame. Plants where a drift ticket is praised (it just saved a rejection) see operators compete to report first. The culture note matters more than the software.
How do running hours get in without machine integration?
The job sheet already records machine hours per shift. A daily or weekly entry into the asset record is enough for hour-based PM; the trigger needs the number, not a live feed.
Does this help with customer audits like BRCGS packaging?
Yes. BRCGS and FMCG customer audits ask for planned maintenance and hygiene-adjacent machine care evidence. Ticket history with PM completion, parts and photos answers those clauses directly.
What about the corona treater and other small equipment?
Register anything whose failure stops or degrades production. The treater that quietly loses treatment level causes lamination failures weeks later; it earns an asset record and a weekly check.
Can it handle seasonal peaks when PM gets skipped?
That is exactly when it earns its keep. Skipped PM is visible as overdue tickets rather than invisible as a chart nobody updated, and the overdue list is the first thing the Monday review reads.
Is this overkill for a two-press plant?
A two-press plant has the most to lose from one press down: half its capacity. The setup is an afternoon, and the drift tickets alone usually pay for the year in avoided rejections.
Bottom line
This week, ask each shift's press operators what they compensated for today. The answers are your unscheduled maintenance backlog, and every one of them is a rejection your customer has not found yet.
This quarter, register the chain as assets, make drift a same-shift ticket, and bolt the inspection checklist onto changeovers. The metric to watch is customer rejections traced to machine wear; as it falls, so does the discounting you never talk about.
Ship rolls, not rejections
VisitorFlow runs maintenance ticketing, PM schedules and asset history on one cloud platform, alongside visitor, gate pass, courier and incident workflows.
Explore Maintenance Software See Material Gate Pass Software Book a Free Demo
Ed Jhonson is a Sourcing & Marketing Expert who writes content related to Technology and Engineering topics.
- From Register Book to Software: Digitizing the Gate Pass
- Inter-Branch Transfer Gate Pass: Keep Stock True Across Units
- Material Inward Gate Pass: Link the Gate with the GRN
- E-Way Bill vs Gate Pass: What Each Document Does
- Gate Pass System for Engineering and Fabrication Workshops
- Gate Pass Software for Pharma and Chemical Plants
- Office Facility Maintenance Checklist: Daily, Weekly, Monthly
- Breakdown Maintenance Log: Record, Analyze, Reduce
- Maintenance KPIs and Dashboards: What to Review Weekly
- AMC Management Software: Contracts, Renewals and Vendor SLAs